 Spanish
 English
 Italian
 Portuguese
 French
Welcome to Our Blog - ITG Group
Blog
- Innovation
- Oct 19, 2026
Buying Second-Hand Machinery Shouldn't Be a Gamble: Introducing ITG Machinery
Buying second-hand machinery should be a smart way to grow. For many mills, it feels more like a bet.
The logic behind it is sound: a second-hand loom or warping machine can bring capacity online faster, with a smaller investment than new equipment. What holds most buyers back isn't the price. It's the question a typical listing never answers: what condition will this machine actually be in when it reaches my factory?
The real problem with the second-hand market
The second-hand machinery market isn't short on offers. It's short on accountability.
A listing tells you the brand, the model, maybe the year. It rarely tells you how the machine was running before it came off the line, whether anyone has checked it since, or who you call if it doesn't perform once it's installed. In many deals, the seller's involvement ends at the transaction, and every risk after that is yours: parts nobody warned you about, a start-up that takes longer than planned, capacity you budgeted for that never shows up.
For a factory owner, that's capital tied up in uncertainty. For a purchasing manager, it's a supplier decision that's hard to defend if it goes wrong. In both cases, the machine itself is rarely the whole problem. The missing backing is.
What changes with ITG Machinery
ITG Machinery is ITG Group's department dedicated to second-hand machinery. It manages the selection and commercialisation of second-hand equipment from start to finish, and the word that matters most there is selection.
Every piece of equipment is evaluated against specific criteria of quality, operation and reliability. Our technical and commercial team assesses each option before it's offered, and each machine is thoroughly inspected so it arrives ready for your production line.
That changes the question you're asking. Instead of “what am I actually getting?”, it becomes “which of these fits my production?”, and you answer it with people who have already looked at the machine.
The platform covers machinery from leading brands such as Picanol, Toyota, Vamatex, Itema, Dornier, Sulzer and many others. Behind it is the same group you may already know from spare parts and new machinery: decades in the textile industry and a distribution network in more than 50 countries.
That's what we mean by second-hand machinery, first-class backing.
The people behind the backing
Backing isn't a policy. It's the people who answer when you have a question.
ITG Machinery is led by Fabio Giamminola, General Director of ITG Brasil, who brings the group's commercial and technical experience to every selection. Alongside him, Vania and Arissa run the administrative and commercial side of the process. They're the team you'll be speaking with from your first inquiry until the offer reaches you.
This matters more than it might seem. When you buy secon-hand equipment, you're not only buying a machine. You're trusting someone's judgement about it, and knowing who that someone is, and being able to reach them, is part of the backing.
How to get started
Everything happens directly on the platform, in three ways:
Buy from the listing. Start by browsing the machines currently available. If you find the reference you're interested in, send your interest request through the platform, and the negotiation starts from there.
Request a search. If the machine you need isn't on the listing, you don't have to stop there. Submit a search request: register your company and describe the machinery you're looking for. The ITG Machinery team will then help you find it.
Sell your machinery. Machinery your mill no longer uses can still be valuable to another one. Register it through the sales form, upload its details and photos, and submit it for publication on the platform, where it can reach thousands of potential buyers in the textile industry worldwide.
Buying second-hand shouldn't mean buying blind
Take a look at the current offer on the ITG Machinery platform, or write to us at itg.machinery@group-itg.com. Tell us what your line needs, and we'll tell you whether we have the right machine for it.
- Textile industry
- Oct 14, 2026
Nextech 2026: Discovering Where the Textile Industry Is Headed
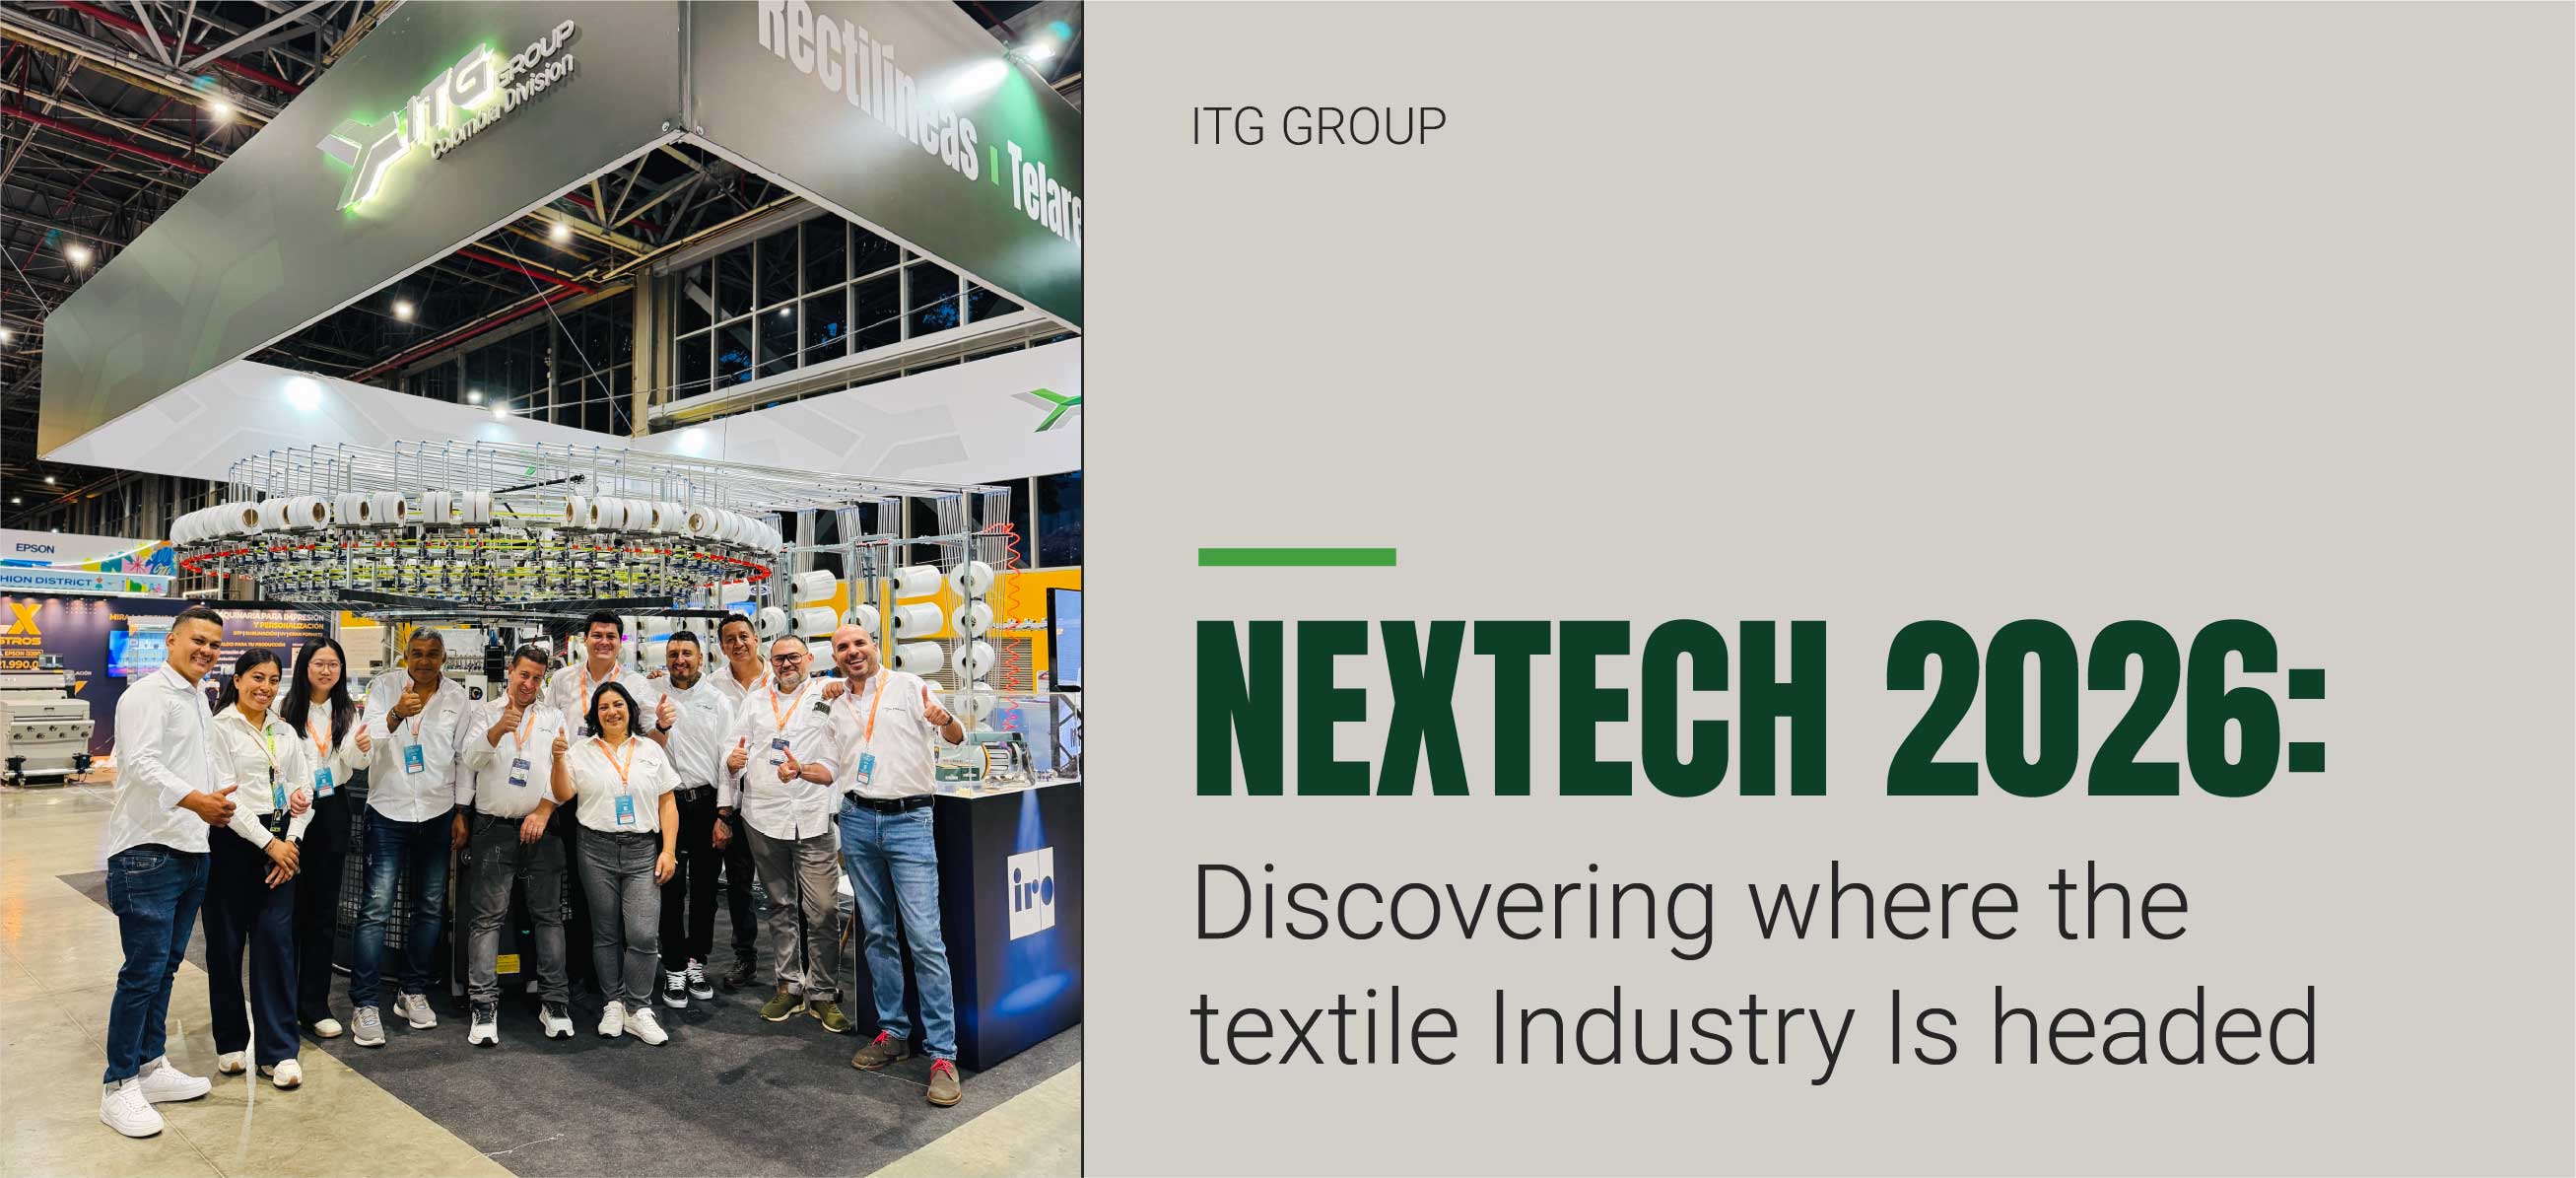
From September 22 to 24, we attended the first edition of Nextech by Colombiatex at Plaza Mayor in Medellín. It is Latin America’s first trade show specializing in machinery and technology for the textile and apparel supply chain. According to Inexmoda, Colombia accounted for 6.8% of the Latin American fashion market in 2025—approximately USD 8,494 million—and the industry is asking itself how to produce better, not just more.
At our booth, we had knitting looms, braiding machines and SINOTEX flat knitting looms in operation. We had visitors from different cities in Colombia, as well as from Ecuador, Peru, Argentina, and Europe, and a good portion of them were companies we hadn’t worked with yet. Almost all conversations revolved around four topics.
Topic 1: Knitting remains the foundation, but growth doesn’t always mean buying another machine
This was the most frequently asked question. Before adding a machine, check if you can diversify with the one you already have:
Change parts, not the machine. On single-knit knitting machines, by changing the core components, the same machine can be converted to knit terry or polo fabric.
Change the gauge with a new cylinder. You can produce a different type of fabric with the same equipment and a much smaller investment than that of a complete machine.
Choose wisely between tubular and open-width knitting. If you work with fabrics containing Lycra or light colors and the fold of the tube leaves marks, the open-width method rolls up the spread-out fabric, preventing those wrinkles and maintaining a uniform stitch density. If you produce garments without side seams, the tubular method remains the most efficient option.
Topic 2: For collars and cuffs, the difference lies in the design
Every technique you master is one more product you can offer: mini jacquard, embossed pleats, intarsia, transfers, or shaped collars. If you’re evaluating a flat knitting machine, keep this in mind:
Rising and lowering rollers: the fabric comes out straight without needing to be hung by hand.
High-heel needles: the cams wear less.
Servo-controlled motor: according to the manufacturer, it increases production by 15%.
Four lancing bars and eight feeders: more colors in a single design.
Topic 3: In braiding, continuity comes down to the details
Braiding is used in shoelaces, sports and safety ropes, fishing line, headphone cables, and jacquard cords, made of polyester, nylon, PP, or Dyneema. If you’re considering a braiding machine:
It’s part of the final product. The number of spindles and heads determines what you can produce and at what rate.
Look for an automatic shut-off in case of thread breakage to avoid accumulating defective lengths. According to the manufacturer, some rope-making models produce 4 to 5 times more than a traditional braiding machine.
Keep consumables close at hand. With spools, carriers, springs, and brake pins readily available, a stoppage lasts hours rather than weeks.
Think about the finishing. If you produce cords, an automatic stitching machine capable of 4,000 to 6,000 stitches per hour completes the process without relying on manual labor.
Topic 4: The cutting room has become a major topic of conversation
Automatic fabric spreading and cutting machines—a line we recently introduced with YINENG TECH—were among the most frequently inquired about. Fabric typically accounts for 60% to 70% of a garment’s cost, and Lectra estimates that waste in cutting rooms ranges from 10% to 20%. It is one of the largest cost centers in a garment manufacturing operation and almost always the least measured.
Before looking at any technical specifications, measure these four things over the course of a typical month: your marking efficiency by garment type, your scraps and rework by cause, the actual hours your cutting table is in use, and your true bottleneck (consistency, setup time, or volume). Also, evaluate spreading and cutting together. An automatic cutting machine only cuts the fabric layout it is fed. If the fabric is still laid out by hand, you’ve automated the precise step and left the imprecise one as it was.
Before Making a Decision
Anyone returning from a trade show comes back with options on the table. These four questions help you sort through them:
What are you going to produce, and for which market?
What is the actual productivity with your yarn and your shifts?
Are replacement parts available nearby?
What does the support for installation, commissioning, and training include?
Most decisions to invest in machinery are made months after a trade show, when there’s time to compare options calmly. We’ve seen this happen in other divisions of the group, which is why we never consider any conversation closed. If you submitted a request, our sales team will reach out to you to help bring it to life. And if you didn’t get a chance to visit us or want to discuss any of these topics for your plant, please write to us.
Thank you to everyone who stopped by to visit us during Nextech.
- Technical
- Sep 08, 2026
Your stenter is burning margin — and you can hear it in the exhaust fan
If you run a finishing line, you already know which machine you'd check first if the energy bill jumped: the stenter.
It's usually the single largest thermal energy consumer on the floor, and the reason is simple physics — you're pushing wet fabric through chambers of hot circulating air, and generating that heat, chamber after chamber, shift after shift, is expensive. The literature is blunt about it: the stenter is described as one of the most thermal-energy-consuming machines in the entire textile process, and finishing together with wet-processing preparation accounts for roughly 35% of a composite mill's thermal energy.
Here's the part that doesn't show up on a gauge: a large share of that energy never touches your fabric. It leaves through the exhaust stack as hot air, radiates into the workshop, or gets wasted holding temperature the process didn't need. That's not a dramatic failure. It's a quiet, continuous leak — and it's paid for in every meter of fabric you run.
This article breaks down where a conventional stenter loses energy, and how the design of our XY-D-2600 Stenter Machine attacks each loss at the source.
Where a conventional stenter loses energy
Three losses account for most of the waste, and they compound.
Hot exhaust air, thrown away. A stenter continuously vents humid, hot air to keep the chamber atmosphere right for drying. In a conventional setup, that exhaust — carrying real thermal energy you already paid to generate — goes straight up the stack. Research on stenter energy flows identifies exhaust gas as one of the single biggest bottlenecks to efficiency, and studies on waste-heat recovery from stenters have demonstrated fuel-consumption reductions above 60% when that exhaust heat is properly captured and reused. Every degree in that vented air is money spent once and lost.
Thermal leakage and radiation. Heat doesn't stay politely inside the chambers. It escapes through panel walls, gaps and poorly insulated surfaces — which is why the area around an older stenter is often uncomfortably hot. That radiated heat is doubly costly: it's energy that left the process, and it raises the workshop temperature, which your ventilation then has to fight.
Temperature and airflow you can't control precisely. When you can't independently regulate conditions across the machine — top versus bottom, section by section — you compensate by overshooting. You run hotter or push more air than the fabric strictly needs, just to hold quality. That safety margin is real fabric quality insurance, but it's also continuous over-consumption. And atmospheric conditions make it worse: energy-model studies show stenter performance can swing by up to 10% of total energy required just from seasonal changes in ambient air temperature and humidity.
How the XY-D-2600 attacks each loss
The XY-D-2600 Stenter Machine is a double-layer stenter built specifically around energy consumption. Three design features map directly onto the three losses above.
1. Double-layer oven — reusing heat instead of regenerating it. This is the core idea. The oven is stacked in two layers, and the heat generated in the first heat-setting layer is transferred to the second layer through a closed iron plate. Instead of every chamber generating its own heat from zero, the second layer runs partly on heat the first layer already produced. Per the catalog, that recovery is worth about 20%–40% energy saving, depending on the process. And because the layers are stacked, each cabinet is 1600 mm high — you get that saving without doubling your floor area.
2. Waste-heat recovery — preheating fresh air with air you were going to vent. The second attack is on that exhaust stack. A stenter constantly needs to replenish fresh air into the oven. In the XY-D-2600, that incoming fresh air is routed through the waste-heat recovery device first — so it's preheated by the outgoing exhaust before it enters the chamber. You're recovering energy from the exact air you were about to throw away. The catalog puts this at roughly 10%–30% energy saving. The exhaust and supplementary fans are both frequency-controlled, and the system reports a 2%–3% production-efficiency gain on the same line, depending on process conditions. The insulation backs it up: panels are galvanized plate with 150 mm of high-quality insulation material to shut down the heat leakage described earlier.
3. Independent dual air ducts — precision instead of overshoot. The third feature solves the over-consumption problem. The XY-D-2600 uses two independent air ducts, with upper and lower air volume controlled separately and settable to any ratio through the menu, regulated by frequency converters. That means you stop compensating with blanket overshoot and start matching airflow to what the fabric actually needs, top and bottom. Critically, this holds even at low speed — which is exactly where sensitive fabrics live. The catalog specifies stable fabric results at any speed for knitwear, coated fabric, recycled fabric, ultra-fine fiber, plush and silk. Lower, precise airflow on delicate goods is both an energy saving and a quality safeguard at once.
What this means on the bill — and in the fabric
The savings percentages above aren't marketing rounding — they're catalog figures tied to process conditions, and they stack on the machine that's already your biggest energy line. When your single largest thermal consumer runs 20%–40% more efficiently in the oven and recovers another 10%–30% from exhaust, that isn't a rounding error on the energy bill. It's a structural change to your cost per meter — the kind that compounds every shift, every day, for the life of the machine.
Independent industry work points the same way: waste-heat recovery projects on stenters have reported 20%–30% savings in electricity and fuel, and broader stenter modernization is credited with cutting specific energy consumption by 10%–25%. We're not going to hand you an ROI figure — that depends on your energy price, your fabric mix and your run hours, and anyone who quotes you a universal payback is guessing. But the direction is not in question, and the inputs to calculate your own are all here.
And the quality side matters just as much, because energy efficiency that costs you fabric quality isn't efficiency. The same features that save energy — precise dual-duct airflow, heated fresh air fed in to avoid large temperature differentials and dripping, stable conditions at low speed — are the features that protect hand feel and finish consistency on sensitive fabrics. On a stenter, done right, the energy decision and the quality decision are the same decision.
Where ITG Group fits
ITG Group supplies the XY-D-2600 double-layer stenter, and our role doesn't end at the purchase order. Sizing a stenter to your line — chamber count, working width, heat source, the fabrics you actually run — is a technical conversation, not a catalog pick. If your current stenter is running hot, venting heat into the workshop, or forcing you to overshoot temperature to hold quality, those are the symptoms worth evaluating.
Tell us what you're finishing and the conditions you're running, and our technical team will work through the configuration with you — including an honest read on whether the numbers justify the change for your specific operation.
Get in touch: info@group-itg.com
- Technical
- Aug 03, 2026
The Frame Problem: How Low-Quality Heald Frames Quietly Drain a Mill's Productivity
Ask any weaving manager what stops their looms, and you'll hear about yarn quality, humidity, machine age. What you'll rarely hear about is the component doing millions of movement cycles right in the middle of it all: the heald frame.
That's a blind spot — because the numbers say frames deserve far more attention than they get.
A study of loom stoppages in an air-jet weaving mill found that 58% of all stops were caused by warp breakages — by far the largest category, ahead of weft breaks (34%) and everything else combined (8%). And here's the detail that matters for this article: where the warp breaks determines how long the loom stays down. A break near the reed can be repaired with a quick knot. A break in the heald and drop wire zone takes significantly longer — the weaver has to identify the affected heald wire, rethread the yarn, and restart.
The same body of research puts the average warp break repair at around 2.87 minutes. That sounds small — until you multiply it across every loom, every shift, every day. A mill running dozens of looms with an elevated warp break rate is losing full production hours daily, one "small" stop at a time.
The heald frame endures millions of high-speed movement cycles, constantly interacting with heald wires and bearing tension from the warp. Research on heald frame design identifies it as one of the loom components most responsible for vibration and noise — and vibration is precisely what limits high-speed performance.
When a frame is poorly built or worn, the chain reaction looks like this:
1. Excess vibration transfers stress to the warp yarns on every shedding cycle.
2. Stressed yarns break more often — feeding that 58% category of stops.
3. Worn or misaligned frames force mills to reduce loom speed just to keep running.
4. Frames that can't hold up wear out faster, doubling replacement frequency — and doubling the downtime each replacement requires.
Industry analysis of weaving components is blunt about it: a poor-quality or worn heald frame doesn't just reduce weaving speed — it causes warp thread breakage, creates defects on the fabric surface, and increases maintenance costs simultaneously.
Every unplanned stop carries three costs at once: lost production, idle labor, and quality risk. That last one is the most underestimated — loom stoppages don't just pause output, they leave startup marks and differential dye take-up woven into the fabric as visible defects. The stop ends; the defect ships.
Industry benchmarks target under 10% total downtime for efficient weaving production. A mill whose frames are quietly inflating its warp break rate can blow through that threshold without a single "major" breakdown ever appearing in the maintenance log.
When a mill audits its downtime, the heald frame rarely gets a line item — the stops get attributed to "warp breaks" and the analysis ends there. But if warp breaks are your biggest stop category, the components touching those yarns thousands of times per minute deserve to be your first inspection point, not your last.
A frame is not a commodity. At production speed, it's the difference between a loom that runs and a loom that stops.
At ITG Group, our heald frames for high-speed air-jet looms are engineered for exactly this: durability, reduced maintenance costs, and stable performance up to 1000 RPM, compatible with Picanol, Toyota and Tsudakoma looms. If recurring stops are eating your production hours, our technical team can help you evaluate whether your frames are part of the problem.
Sources: Austin Journal of Textile Engineering (loom stoppage study); research on heald shaft design and vibration (composite heald frame studies); VieTextile component selection analysis; Textile School downtime benchmarks.